Plasma ammonia synthesis — 85 hours running, but cheaper fertilizer?
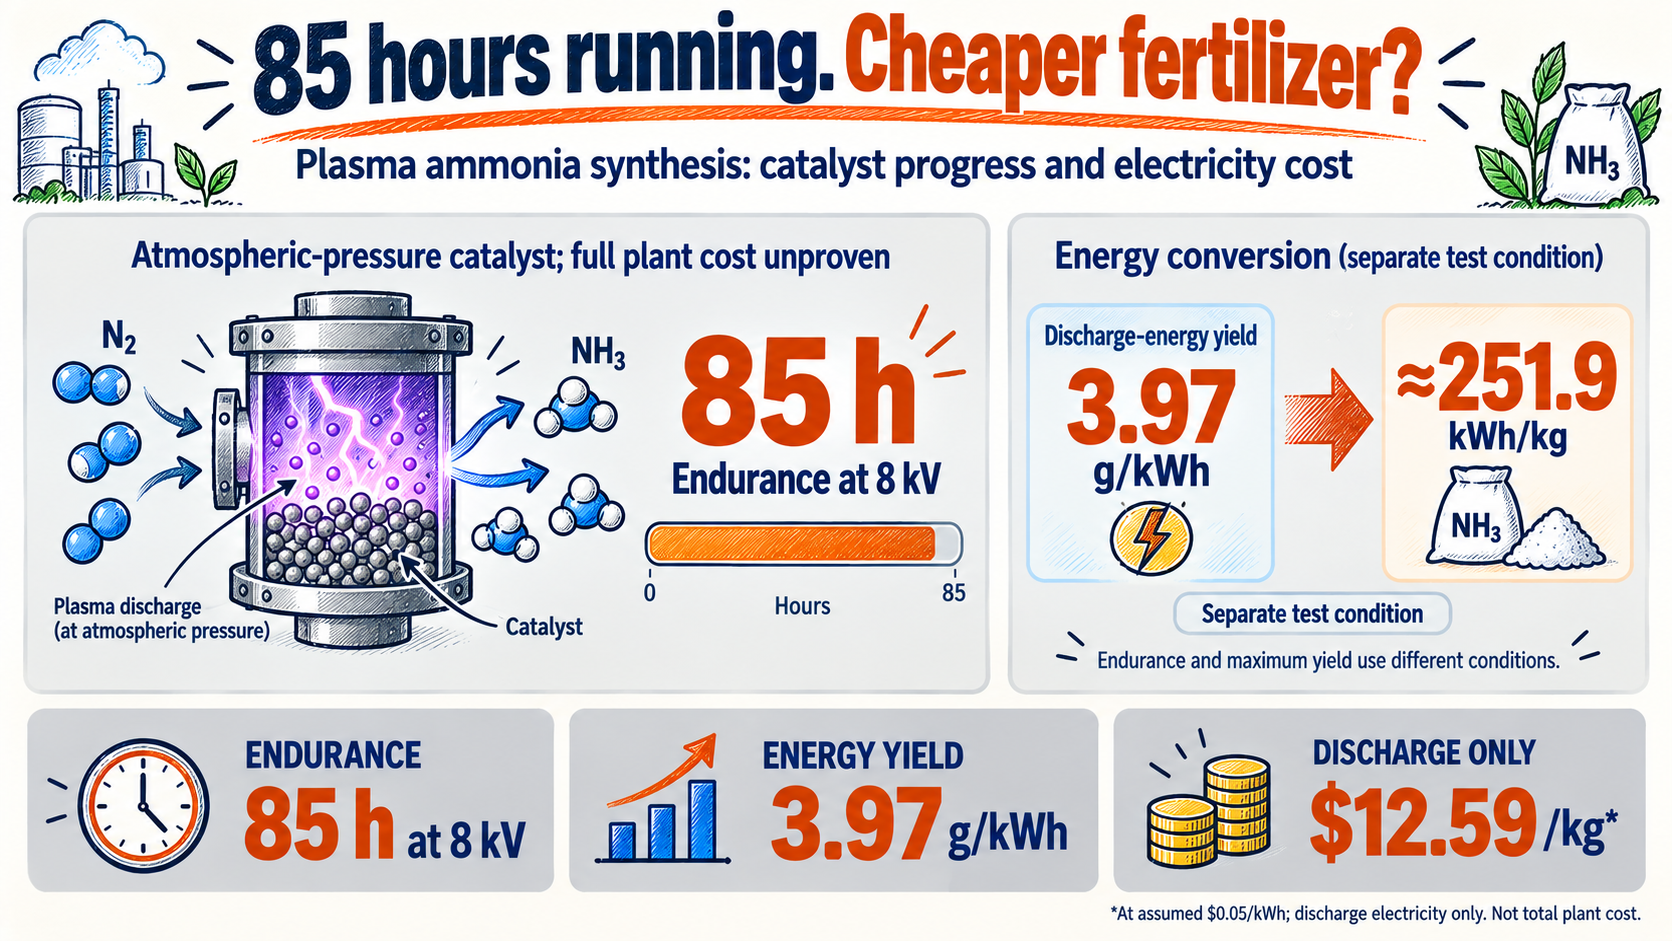
Plasma ammonia synthesis has a new catalyst that operated continuously for 85 hours at atmospheric pressure. That is encouraging for smaller production systems. It does not establish cheaper fertilizer. The useful question is how a materials advance could change production costs—and which costs it leaves unresolved. Nature Communications paper
Ammonia combines nitrogen and hydrogen and is a starting material for nitrogen fertilizers. Changes in its production costs can therefore reach agriculture. The International Energy Agency’s 2021 roadmap put fertilizer use at around 70% of ammonia demand. This is a dated industry reference, not a fresh measurement of the 2026 market. IEA ammonia roadmap
Niu and colleagues published the study in Nature Communications on September 10, 2026. It is a peer-reviewed article in press, awaiting final editing. Experimental findings, company announcements and the economic reasoning below have different evidential status; the cost scenarios are our calculations. Paper and publication status
What does plasma ammonia synthesis change?
Nitrogen molecules are difficult to convert because their two atoms are tightly bonded. Conventional Haber–Bosch production combines nitrogen and hydrogen over a catalyst at elevated temperature and pressure. A catalyst makes a reaction easier to accomplish. Decades of large-scale operating experience give this incumbent process an advantage that a lower-pressure reactor alone cannot erase. Incumbent production and transition pathways: IEA
In a nonthermal plasma, energetic electrons can help initiate chemistry without heating all the gas to the same high temperature. The aim is to combine that electrical activation with useful reactions at a catalyst surface. A mild bulk temperature describes the operating conditions; it does not tell us how much electricity is consumed per kilogram of product.
The experiment uses supplied nitrogen and hydrogen gases. An integrated plant would still need feedstock preparation and product recovery. Those operations must enter the business case even when the synthesis reactor operates at atmospheric pressure. Manuscript: feed gases and reactor conditions
Conventional Haber–Bosch
Elevated temperature, pressure and catalyst
Activation
Operating base · Established large-scale operation
Cost boundary · Feedstocks, synthesis, recovery, capital
This plasma study
Electrical discharge and a new Pt catalyst
Activation
Test conditions · Atmospheric pressure; supplied N₂ and H₂
Still to establish · Complete cost of saleable product
The advance is in how the platinum is arranged
The materials advance is a plasma-based preparation method at the boundary between two immiscible liquids. It stabilizes isolated platinum atoms together with small platinum clusters on nitrogen-containing carbon, addressing nitrogen loss and metal migration during conventional thermal preparation. Paper: catalyst preparation
The proposed mechanism assigns different roles to the isolated atoms and clusters in nitrogen activation and hydrogen supply. Spectroscopy, isotope experiments and calculations support this interpretation. It is a mechanistic proposal, rather than a direct observation of every surface reaction. Paper: proposed cooperative mechanism
The engineering implication is that catalyst qualification should examine the arrangement and persistence of active sites, not just the amount of metal purchased. If a manufacturer can reproduce a useful arrangement across batches, structural consistency becomes a potential source of value. That is an industrial inference, and achieving it at manufacturing scale remains a separate task.
Higher concentration, with a limited endurance demonstration
At 9 kV, outlet ammonia concentration was 2.13% with the new catalyst, versus 0.48% with the commercial platinum-on-carbon comparator. Applied voltage and gas flow matched; discharge power and platinum loading did not. This comparison does not establish a corresponding improvement in energy efficiency or production cost. Manuscript Figure 4a and experimental discussion
Source: Figure 4a. Same applied voltage and gas flow; discharge power and Pt loading differ. Not a cost or product-purity comparison.
A more concentrated outlet can potentially reduce the gas-handling burden for a given amount of ammonia. But an experimental product stream is not a saleable product. Recovery yield, purity and energy for handling unreacted gas must be measured before assigning a saving. Better reactor chemistry creates an opportunity for process design; it does not finish that design.
The 85-hour endurance test was conducted separately at 8 kV. It does not certify that duration at the maximum-energy-yield condition. A prospective buyer would next ask about repeated starts, feed impurities, cleaning and replacement downtime. Continuous laboratory operation answers only part of an equipment procurement question. Manuscript Figure 4h: endurance conditions
What 3.97 grams per kWh means for the electricity bill
The reported energy yield is 3.97 grams of ammonia per kWh of discharge energy. Supplementary Equation S6 explicitly uses discharge power in its denominator. This is a reactor metric, not a complete plant electricity-meter reading. Supplementary Note 2, Equation S6
Inverting the yield gives 1,000 ÷ 3.97, or approximately 251.9 kWh per kilogram. At an assumed electricity price of $0.05/kWh, the discharge-energy component would be about $12.59/kg. This is our illustrative calculation, not a techno-economic assessment reported by the authors.
Using assumed tariffs of $0.03, $0.05 and $0.10/kWh produces discharge-energy costs of approximately $7.56, $12.59 and $25.19/kg. These are scenarios, not quoted electricity tariffs or ammonia market prices. They hold the experimental yield constant to isolate the effect of electricity price.
Calculation: (1,000/3.97) × assumed tariff. Excludes feedstocks, power losses, recovery, catalyst and capital. Not total cost or market quotations.
The figures exclude power-supply losses, hydrogen and nitrogen production, ammonia recovery, catalyst replacement and capital costs. Adding these items would change the delivered cost. The calculation therefore exposes an engineering priority: improve output per unit of electrical energy while retaining the useful catalyst structure.
Comparisons with conventional plants need consistent boundaries. IEA plant energy figures incorporate feedstock and fuel and may use net-energy accounting. Dividing them directly into a laboratory discharge-energy figure would not provide a clean efficiency comparison. The commercial comparison should deliver the same product purity to the same location and account for all required equipment. IEA: plant energy and incumbent assets
The competitors are already changing their plants
Yara’s 2025 annual report describes its 24 MW renewable-hydrogen demonstration facility at Herøya as operational. It states that full capacity can support roughly 20,000 tonnes of renewable ammonia annually. Capacity is not evidence that this volume was actually produced. Yara Annual Report 2025
On September 7, 2026, Yara announced the inauguration of its Sluiskil carbon-capture facility. The company reports capacity to capture and liquefy up to 800,000 tonnes of CO₂ annually from ammonia production, with Northern Lights providing transport and storage. This is a capacity announcement, not a full year of verified capture. Yara September 7 inauguration announcement
Neither project uses the new plasma catalyst. One changes hydrogen supply; the other manages carbon emissions. Yet they can compete for the same customer budgets. When a producer can improve an existing asset, a new synthesis platform needs a compelling advantage in total cost, location or operating flexibility.
The paper cannot establish when existing ammonia plants might be displaced or how much a particular supplier’s revenue could grow. Commercial diligence needs sustained saleable output, equipment cost, power contracts and customer commitments. This analysis does not recommend buying or selling a security.
A first market could depend on location rather than scale
One conditional opportunity is smaller production close to users who face substantial transport and storage costs. A local unit could compete against delivered cost rather than a large plant’s gate price. This is a possible business model inferred from the technology, not one validated by the experiment.
Operating only during cheap-power hours introduces another trade-off: fewer running hours spread fixed equipment costs across less product. Hydrogen availability and product storage must also fit the operating schedule. A promising location would combine inexpensive electricity, sufficient utilization and reliable nearby demand.
-
1
Location
Affordable power and hydrogen; nearby users
-
2
Process performance
Adequate utilization, recovery and catalyst life
-
3
Customer economics
Compare delivered cost including avoided transport
If these conditions are met, demand could extend beyond catalysts and power supplies to recovery modules, product measurement and maintenance services. Productivity must also be measured over a useful operating period. Faster chemistry does not necessarily increase annual shipments when cleaning or replacement interrupts production. Customers ultimately pay for dependable quantities of specification-compliant product.
For Korean readers, changing fertilizer sourcing and changing fertilizer production technology are distinct strategies. Our separate discussion of potash examines sourcing. Potassium is a different plant nutrient from nitrogen; an ammonia synthesis advance cannot substitute for potash. Related: potash sourcing and pricing
What would make the next result commercially stronger?
The next commercially useful evidence would include full-process energy consumption, repeat operation at larger scale and product costs that include catalyst replacement. Scaling should preserve both the material structure and useful reactor performance. A larger vessel alone would not demonstrate that.
My assessment is that the immediate significance lies in catalyst design, while the commercial opportunity depends on better electrical yield and product recovery. The route from an 85-hour experiment to an operating business will be judged by the complete bill for a kilogram that a customer can actually use.
Commercial progress must reduce the complete cost of a kilogram of ammonia delivered to a customer.
Sources and further reading
- Niu et al., Nature Communications (2026), DOI: 10.1038/s41467-026-77160-5
- Nature Communications accepted manuscript, pp. 9–11 / Fig. 4
- Supplementary Information, Note 2 / Tables S4–S5
- IEA, Ammonia Technology Roadmap (2021)
- IEA, Executive Summary (2021)
- Yara Annual Report 2025
- Yara, Sluiskil carbon capture inauguration (2026-09-07)
For information only — this is not a recommendation to buy or sell any asset.
Comments 0