암모니아 수소 추출, 250℃로 낮추고 4배 빨라졌다 — Nature 전기화학 막 해부Ammonia Hydrogen Extraction at 250°C — Inside Nature’s 4× Electrochemical Membrane
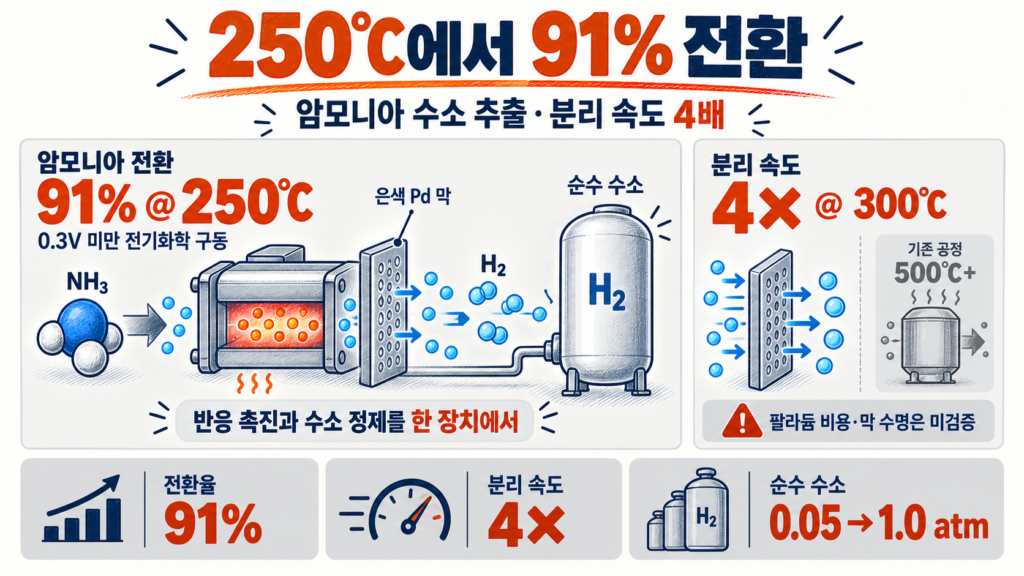
암모니아 수소 추출 기술에 꽤 의미 있는 숫자가 나왔습니다. 2026년 9월 9일 Nature에 실린 MIT 연구는 250℃에서 암모니아를 최대 91% 전환했고, 300℃에서는 기존 압력 구동 방식보다 수소 분리 속도를 4배 높였습니다. 반응과 정제를 한 장치에서 처리했다는 점이 더 중요합니다. 무엇이 달라졌는지, 그리고 수소 운송비를 낮추려면 무엇을 더 증명해야 하는지 구분해 보겠습니다.
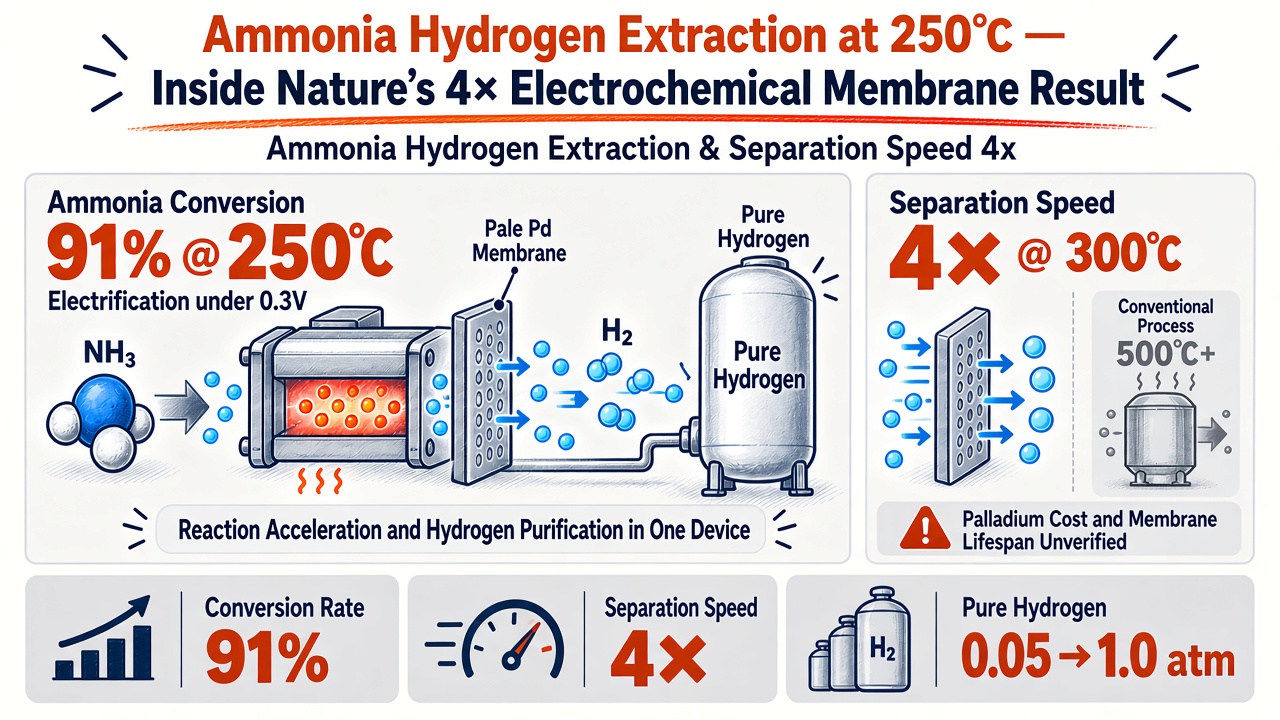
Ammonia hydrogen extraction just produced a set of unusually consequential numbers. A Nature paper published on 9 September 2026 reports up to 91% ammonia conversion at 250°C and a fourfold increase in hydrogen-separation rate at 300°C versus pressure-driven operation. More importantly, the device promotes the reaction and purifies hydrogen in one unit. This article explains what changed and what still has to be proven before the idea can lower delivered hydrogen costs.
먼저 선을 그어야 합니다. 이것은 상업 플랜트의 원가 절감 보고서가 아니라 실험실 규모의 개념증명입니다. 논문이 확인한 것은 온도·전환율·분리 성능입니다. 설비비 절감, 항만 시장 확대, 기업 수혜는 그 성능이 큰 장치에서도 오래 유지된다는 조건을 붙인 전망입니다.
암모니아 수소 추출이 왜 어려웠을까요?
수소는 가볍지만 운반하기는 까다롭습니다. 같은 양의 에너지를 멀리 보내려면 기체를 높은 압력으로 눌러 담거나 영하 253℃ 부근까지 식혀 액체로 만들어야 합니다. 압축에는 에너지가 들고, 액화에는 극저온 탱크와 냉각 설비가 필요합니다.
그래서 수소를 암모니아(NH₃)에 화학적으로 넣어 운반하는 방법이 주목받습니다. 암모니아는 이미 비료 원료로 세계 곳곳에서 생산되고 배로 운송됩니다. 문제는 도착지에서 다시 수소를 꺼내는 ‘크래킹’입니다. MIT 설명에 따르면 높은 반응속도와 전환율을 얻으려면 보통 500℃가 넘는 온도가 필요합니다. 나온 기체에는 수소뿐 아니라 질소와 반응하지 않은 암모니아도 섞여 있어 후단 정제도 거쳐야 합니다.
쉽게 말해 택배 상자는 잘 왔는데, 포장을 뜯고 내용물을 깨끗하게 골라내는 데 돈이 많이 드는 상황입니다. 크래커를 달구는 열, 정제 장치, 압축기, 안전 설비가 모두 최종 수소 가격에 붙습니다. 암모니아가 해상 운송에 유리해도 마지막 회수 단계가 비싸면 전체 계산은 다시 흔들립니다.
-
1
암모니아 운송
액체 저장·운송
-
2
500℃+ 크래킹
수소+질소 생성
-
3
후단 정제
잔류 NH₃ 제거
-
4
고순도 수소
압축·사용
전기화학 팔라듐 막은 기존과 뭐가 다를까요?
기존 팔라듐 막도 수소만 통과시키는 성질을 이용했습니다. 다만 보통 막 양쪽의 수소 압력 차가 이동을 만듭니다. 수소 농도가 낮거나 회수하는 쪽 압력이 높아지면 밀어내는 힘이 약해집니다. 막을 얇게 만들면 흐름은 빨라지지만 기계적 안정성이 나빠질 수 있습니다.
새 장치는 팔라듐 기반 막을 전기화학 셀의 양극으로 바꿨습니다. 막 반대편에는 녹인 수산화물 전해질과 수소 발생 음극이 있습니다. 막에 도착한 수소는 양성자와 전자로 나뉘어 서로 다른 길로 이동한 뒤, 반대쪽에서 다시 순수한 수소 기체로 합쳐집니다.
은 압력차가 아니라 전압으로 수소를 끌어당긴다는 점입니다. 연구진은 이를 수소에만 작동하는 능동 펌프처럼 만들었습니다. 0.3V 미만의 낮은 양극 전위에서도 막을 통한 이동이 확산 한계에 이를 만큼 빨랐습니다. 수소가 5%만 들어 있는 혼합기체, 즉 수소 분압 0.05기압에서 출발해 1기압의 순수 수소 흐름을 얻었습니다.
-
1
촉매 반응
NH₃에서 H₂ 방출
-
2
Pd 막 양극
수소만 선택
-
3
전기화학 이동
0.3V 미만 구동
-
4
순수 H₂ 재결합
1기압 흐름
여기서 막은 필터 이상의 일을 합니다. 암모니아가 분해되며 생긴 수소를 바로 빼내면, 생성물이 쌓여 반응을 방해하는 현상이 줄어듭니다. 욕조의 물을 계속 퍼내면 수도꼭지에서 들어오는 물이 더 쉽게 자리를 차지하는 것과 비슷합니다. 화학에서는 르샤틀리에 원리로 설명합니다. 생성물을 제거하면 평형이 생성물 쪽으로 더 움직입니다.
그 결과 촉매와 막을 붙인 장치는 250℃에서 암모니아를 최대 91% 전환했습니다. 액상 유기수소운반체(LOHC) 후보인 메틸시클로헥산도 최대 94% 전환했습니다. 300℃ 분리 실험에서는 압력으로 미는 방식보다 수소 분리 속도가 4배였습니다. 이 수치는 각각 다른 실험 조건에서 나온 값이므로 ‘모든 공정이 동시에 4배 좋아졌다’고 읽으면 안 됩니다.
비용은 어디서 줄어들 수 있을까요?
상용화된다면 가장 먼저 줄일 수 있는 부담은 열입니다. 반응 온도가 500℃ 이상에서 200~300℃대로 내려가면 고온 버너, 단열재, 내열 부품의 부담을 줄일 여지가 생깁니다. 공장이나 선박에서 나오는 중저온 폐열을 보조 열원으로 쓰기도 쉬워집니다. 다만 새 장치는 전기를 쓰므로 절감한 열에너지와 추가 전력소비를 함께 계산해야 합니다.
공정 통합도 절감 경로입니다. 지금은 ‘분해→불순물 제거→수소 정제→필요하면 압축’이 여러 설비로 이어집니다. 반응기 안에서 수소를 선택적으로 꺼내 고순도 흐름으로 만들 수 있다면 정제탑과 배관, 압축 부하 일부를 줄일 가능성이 있습니다. 장치 수가 줄면 부지와 정비 지점도 줄어듭니다. 특히 항만·충전소·반도체 공장처럼 공간과 수소 순도가 중요한 곳에서 가치가 커질 수 있습니다.
생산성 측면도 있습니다. 수소를 즉시 제거해 반응이 계속 앞으로 가면 같은 전환량을 위해 더 큰 반응기나 반복 순환을 쓰는 부담이 낮아질 수 있습니다. 수소를 생산지에서 기체로 멀리 옮기는 대신 암모니아로 운반하고 소비지 가까이에서 꺼내 쓰는 분산형 모델도 쉬워질 수 있습니다.
기존 열·압력 중심
온도 · 보통 500℃+
분리 · 압력차+후단 정제
설비 · 다단 공정
비용 변수 · 열·정제·압축
전기화학 Pd 막
온도 · 실험 250℃
분리 · 능동 추출+동시 정제
설비 · 통합 가능성
새 비용 변수 · 전력·Pd·막 수명
여기까지는 공학적으로 가능한 절감 경로입니다. 논문은 수소 1kg당 비용, 설비 투자비, 전 과정 효율을 제시하지 않았습니다. 따라서 ‘수소 가격을 몇 % 낮춘다’는 숫자는 아직 붙일 수 없습니다. 실제 원가는 암모니아 가격, 전기요금, 팔라듐 사용량, 막 교체 주기, 촉매 수명과 가동률이 결정합니다.
산업은 이미 암모니아 크래킹에 돈을 넣고 있습니다
연구실 밖의 움직임은 빠릅니다. Air Liquide는 2025년 11월 벨기에 앤트워프-브뤼헤항에서 하루 30톤의 암모니아를 처리하는 산업 규모 파일럿을 가동했다고 밝혔습니다. thyssenkrupp Uhde와 Uniper도 독일 대형 실증 설비를 2026년 말 가동하는 일정을 제시했습니다. 이 회사들의 장치가 Nature 논문과 같은 방식은 아닙니다. 중요한 점은 ‘암모니아에서 수소를 회수하는 설비’가 이미 플랜트 경쟁의 대상이 됐다는 사실입니다.
더 직접적인 비교 대상은 EU의 COUPLE 프로젝트입니다. 이 사업은 팔라듐 막 반응기와 양성자 세라믹 전기화학 반응기를 결합해 하루 100kg의 고순도·가압 수소를 5,000시간 생산하는 실증을 추진합니다. 2026년부터 2028년까지 EU 기여금은 약 600만 유로입니다. Nature 연구와 설계는 다르지만, 막 분리·전기화학·압축·열관리를 한 시스템으로 묶으려는 산업 방향은 닮았습니다.
한국에도 연결점이 있습니다. KBR과 이수화학은 2023년 양해각서를 체결하고 울산에서 하루 10톤 규모 수소 생산용 상업 크래킹 설비 계획을 발표했습니다. JERA와 삼성물산은 2026년 7월 한일 수소·암모니아 가치사슬의 공급 안정성과 저장 운영을 함께 검토하는 양해각서를 맺었습니다. 한국과 일본처럼 에너지 수입 비중이 높은 나라에서는 항만에서 암모니아를 받고 필요한 곳에서 수소를 뽑는 기술이 공급망 선택지를 늘릴 수 있습니다.
이 흐름은 폐열 기반 냉각 기술과도 맞닿아 있습니다. 저온화된 크래커가 산업 폐열을 활용할 수 있다면 에너지 통합의 가치가 커지기 때문입니다. 고순도 수소 수요 측면에서는 AI 반도체 공급망과 제조 공정도 관련이 있습니다. 다만 어떤 기업이 실제 공급 계약을 따낼지는 막 소재와 장치의 상용 성능이 확인된 뒤 판단해야 합니다.
수소 수요 1억 톤인데 깨끗한 수소는 1% — IEA가 보여주는 현실
IEA에 따르면 2025년 세계 수소 수요는 1억 톤을 넘었습니다. 그런데 저배출 수소 생산은 약 100만 톤, 전체의 약 1% 수준입니다. 수요 대부분은 정유와 화학처럼 기존 산업에서 나옵니다. ‘수소 시장이 없다’기보다 깨끗한 수소를 경쟁력 있는 가격으로 공급하는 시장이 아직 작다는 뜻입니다.
투자 열기도 그대로 이어지지는 않았습니다. IEA가 본 2030년 저배출 수소 프로젝트 파이프라인은 발표 기준 2,700만 톤이지만, 실제 가동 가능성이 높은 물량은 이전 평가 1,000만 톤에서 600만 톤 조금 넘는 수준으로 줄었습니다. 비용, 확실한 구매 계약, 규제와 인프라가 부족해 프로젝트가 밀리거나 취소됐기 때문입니다.
바로 이 지점에서 회수 기술이 중요해집니다. 저렴한 재생에너지가 있는 곳에서 암모니아를 만들고 기존 선박·저장망으로 옮긴 뒤, 수요지에서 수소를 효율적으로 꺼낼 수 있다면 생산지와 소비지를 연결하는 비용이 낮아질 수 있습니다. 반대로 크래킹 비용이 충분히 내려가지 않으면 암모니아는 비료나 직접 연료로 쓸 때는 유리해도 수소 운반체로서는 경쟁력이 약해집니다.
상용화 전에 반드시 확인할 네 가지
가장 큰 숙제는 팔라듐입니다. 팔라듐은 수소를 잘 통과시키지만 비싼 귀금속입니다. 연구진도 막에 들어가는 팔라듐 양을 줄이는 연구를 진행 중이라고 밝혔습니다. 막을 얇게 만들거나 다른 금속과 합금화했을 때 성능과 수명이 함께 유지되는지가 원가의 출발점입니다.
- 내구성: 수천 시간 동안 열을 올리고 내리는 운전에서도 막이 갈라지거나 성능이 떨어지지 않아야 합니다.
- 불순물: 잔류 암모니아와 공정 오염물이 촉매·막을 망가뜨리는지, 연료전지급 순도를 계속 유지하는지 확인해야 합니다.
- 전체 효율: 낮아진 열 사용량에서 전기화학 펌프의 전력소비와 보조 장치 손실을 뺀 순효율이 좋아야 합니다.
- 규모와 안전: 막 면적을 키웠을 때 처리량이 선형으로 늘고, 독성 암모니아를 항만·도심 근처에서 안전하게 다룰 수 있어야 합니다.
투자 관점에서는 논문 발표보다 다음 이정표가 중요합니다. 첫째, kg/day가 아니라 ton/day급 모듈의 처리량입니다. 둘째, 5,000시간 이상 연속 운전 자료입니다. 셋째, 수소 순도와 암모니아 잔류량입니다. 넷째, 암모니아 원료비를 제외한 수소 1kg당 회수비용입니다. 이 네 숫자가 공개돼야 기존 크래커·액화수소·다른 운반체와 제대로 비교할 수 있습니다. 이 글은 특정 종목·자산의 매수·매도를 추천하지 않습니다.
논문이 증명한 것, 아직 전망인 것
확인된 사실은 분명합니다. 낮은 전압으로 팔라듐 막을 능동 구동했고, 희석된 수소를 1기압 순수 흐름으로 농축했으며, 250℃에서 암모니아와 메틸시클로헥산의 높은 전환율을 보였습니다. 반응을 촉진하면서 동시에 분리한다는 공정 설계가 작동했습니다.
아직 전망인 부분도 분명합니다. 설비가 작아지고 수소 회수비용이 내려갈 가능성, 항만·분산형 발전·충전소·반도체 공장에 새 시장이 생길 가능성, 기존 고온 크래커와 정제 장치 일부를 대체할 가능성입니다. 모두 팔라듐 사용량과 장기 내구성, 실제 전력소비가 상업 조건에서 맞아야 현실이 됩니다.
제 판단으로 이 연구의 가치는 ‘수소를 더 많이 만들었다’는 데 있지 않습니다. 운반체에서 수소를 꺼내는 마지막 공정을 열과 압력만의 문제가 아니라 전기화학적으로 제어할 수 있게 만든 데 있습니다. 수소경제의 승부는 생산량 발표보다 최종 소비지까지 도착한 수소의 가격에서 납니다. 이번 논문은 그 마지막 가격표를 낮출 새로운 설계도를 보여줬습니다.
250℃와 4배는 과학의 숫자입니다. 사업의 숫자는 막 수명, 전력소비, 처리량과 수소 1kg당 회수비용입니다.
출처와 참고 링크
- Nature — Anodic Pd membrane H₂ extraction enhances thermochemical dehydrogenation
- MIT News — An electrochemical approach turns ammonia into pure hydrogen
- IEA — Global Hydrogen Review 2026, Executive summary
- EU Clean Hydrogen Partnership — COUPLE project
- Air Liquide — Ammonia cracking industrial-scale pilot
- thyssenkrupp Uhde — Ammonia cracking demonstration
- JERA — Hydrogen and ammonia value-chain MoU with Samsung C&T
- KBR — Ammonia cracking unit with ISU Chemical
The boundary matters. This is a laboratory proof of concept, not a commercial cost report. The paper establishes temperature, conversion and separation performance. Lower capital costs, new port markets and corporate beneficiaries remain conditional forecasts.
Why is extracting hydrogen from ammonia so difficult?
Hydrogen is light but awkward to move. Shipping useful quantities requires high-pressure compression or cooling close to −253°C for liquefaction. Both routes consume energy and need specialized equipment.
Ammonia offers another route. It already moves globally as a fertilizer feedstock and can carry hydrogen in chemical bonds. The difficult step comes at the destination: cracking ammonia back into nitrogen and hydrogen. Conventional systems generally need temperatures above 500°C for high rates and conversion, while the product stream still requires purification to remove nitrogen and residual ammonia.
In practical terms, the package travels well but is expensive to open and sort. Heat, purification, compression and safety equipment all appear in the delivered price of hydrogen. A cheap voyage does not solve the economics if recovery at the destination remains costly.
-
1
Ship ammonia
Liquid storage
-
2
Crack above 500°C
H₂ + N₂ produced
-
3
Downstream cleanup
Remove residual NH₃
-
4
Pure hydrogen
Compress and use
How does the electrochemical palladium membrane differ?
Conventional palladium membranes also exploit palladium’s ability to pass hydrogen selectively. They usually rely on a difference in hydrogen partial pressure across the membrane. The driving force weakens when hydrogen is dilute or the recovery side reaches a higher pressure, while thinner high-flux membranes may sacrifice mechanical stability.
The MIT device turns a palladium-based membrane into the anode of a molten-hydroxide electrochemical cell. Hydrogen arriving at the membrane separates into protons and electrons. They travel through the electrolyte and external circuit, respectively, then recombine at the cathode as pure hydrogen gas.
Voltage, rather than a pressure gradient, pulls the hydrogen across. The researchers reached diffusion-limited transport at an anode potential below 0.3 V. They enriched hydrogen from a mixture with a hydrogen partial pressure of 0.05 atmosphere into a pure stream at 1 atmosphere.
-
1
Catalytic reaction
H₂ released from NH₃
-
2
Pd membrane anode
Selects hydrogen
-
3
Electrochemical transfer
Driven below 0.3 V
-
4
Pure H₂ reforms
1-atm stream
The membrane also changes the reaction. Removing hydrogen as soon as it forms reduces product inhibition and shifts the equilibrium toward further dehydrogenation. The membrane is therefore an active pump, not merely a filter.
Coupled to catalysts, the device achieved up to 91% ammonia conversion and 94% methylcyclohexane conversion at 250°C. At 300°C, hydrogen separation was four times faster than in pressure-driven operation. Those results came from distinct experimental conditions; they do not mean every part of a commercial process becomes four times better.
Where could costs fall?
Heat is the most immediate possible saving. Moving from above 500°C toward 200–300°C could reduce demands on burners, insulation and high-temperature components. It could also make industrial waste heat more useful. The device consumes electricity, however, so any fair comparison must subtract electrochemical power use from thermal savings.
Process integration offers another route to lower costs. Today’s chain can include cracking, contaminant removal, hydrogen purification and compression. Selective extraction inside the reactor could eliminate or shrink some downstream equipment, piping and maintenance points. That matters most where footprint and purity carry a premium, including ports, refuelling depots and semiconductor plants.
Productivity could improve as well. Immediate hydrogen removal may deliver more conversion from a smaller reactor and reduce recycle loads. It could also support distributed production: carry ammonia over long distances, then recover hydrogen near the point of use.
Heat and pressure led
Temperature · Typically above 500°C
Separation · Pressure + cleanup
Equipment · Multiple stages
Cost driver · Heat, cleanup, compression
Electrochemical Pd membrane
Temperature · 250°C experiment
Separation · Active pump + purification
Equipment · Potential integration
New cost driver · Power, Pd, membrane life
These are engineering pathways, not measured savings. The paper does not report cost per kilogram, plant capital expenditure or full-system efficiency. Ammonia and electricity prices, palladium loading, membrane replacement, catalyst life and utilization will decide the commercial outcome.
Industry is already funding ammonia cracking
Commercial activity is moving ahead. Air Liquide says it commissioned an industrial-scale pilot in Antwerp-Bruges in November 2025 with capacity to crack 30 tonnes of ammonia per day. thyssenkrupp Uhde and Uniper target the end of 2026 for a large German demonstration plant. These are not the same technology as the Nature device. They show that ammonia-to-hydrogen recovery is already becoming a field of plant competition.
The EU-funded COUPLE project is a closer industrial analogue. It combines palladium membrane reactors with proton-ceramic electrochemical reactors and targets 100 kg of high-purity, pressurized hydrogen per day for 5,000 hours. The 2026–2028 project has nearly €6 million in EU support. Its architecture differs, but its integration of membranes, electrochemistry, compression and heat management points in a similar direction.
There is a Korean connection as well. KBR and ISU Chemical signed a memorandum in 2023 and announced plans for a commercial Ulsan ammonia-cracking unit producing 10 tonnes of hydrogen per day. JERA and Samsung C&T signed a July 2026 memorandum to explore more resilient hydrogen and ammonia value chains. For import-dependent Japan and Korea, recovering hydrogen near ports or industrial users could add a valuable supply option.
The engineering logic connects with our earlier analysis of waste-heat-driven cooling: a lower-temperature cracker may have more opportunities for heat integration. On the demand side, our AI semiconductor supply-chain guide explains why high-purity process gases matter. Actual winners cannot be identified until membrane and system performance are demonstrated at scale.
Hydrogen demand tops 100 million tonnes, but clean supply is 1%
Global hydrogen demand exceeded 100 million tonnes in 2025, according to the IEA. Low-emissions supply was only about 1 million tonnes. Most demand still comes from refining and chemicals. The missing market is not hydrogen itself; it is competitively priced low-emissions hydrogen.
Investment momentum has also weakened. The IEA counts 27 million tonnes of announced low-emissions production for 2030, but projects committed or judged likely to operate fell from 10 million tonnes in the previous assessment to just over 6 million tonnes. Costs, uncertain offtake, regulation and infrastructure are delaying projects.
Recovery technology sits directly inside that gap. Ammonia could connect low-cost renewable production regions with demand centres through established shipping and storage practices. If cracking remains expensive, however, ammonia may be attractive as fertilizer or direct fuel while losing ground as a hydrogen carrier.
Four tests before commercialization
Palladium is the first obstacle. It passes hydrogen extremely well but is an expensive precious metal. The team is working to reduce palladium loading. Any thinner or alloyed membrane must preserve both performance and life.
- Durability: membranes must survive thousands of hours and repeated thermal cycling without cracking or losing flux.
- Contaminants: catalysts and membranes must tolerate process impurities while keeping residual ammonia within end-use specifications.
- Net efficiency: saved heat must exceed the electricity and balance-of-plant losses introduced by electrochemical pumping.
- Scale and safety: throughput must rise with membrane area, while toxic ammonia is handled safely near ports and demand centres.
The most useful milestones are therefore tonnes per day, more than 5,000 hours of continuous operation, verified hydrogen purity and residual ammonia, and recovery cost per kilogram excluding ammonia feedstock. Those figures will permit a real comparison with conventional crackers, liquid hydrogen and other carriers. This article does not recommend buying or selling any security or asset.
What the paper proves—and what remains a forecast
The demonstrated facts are strong: low voltage actively drove hydrogen through a palladium membrane, dilute hydrogen became a pure 1-atmosphere stream, and high conversion of ammonia and methylcyclohexane occurred at 250°C. Reaction promotion and separation worked together.
The economic claims remain conditional. Smaller plants, lower recovery costs, new markets at ports and distributed users, and partial displacement of high-temperature crackers and purification equipment all depend on palladium loading, long-term durability and real power consumption.
The research matters less because it makes more hydrogen than because it changes the final recovery step from a problem governed mainly by heat and pressure into one that can be controlled electrochemically. Hydrogen economics are decided by the cost of usable gas at the customer’s site. This paper offers a new design for reducing that final price tag.
250°C and 4× are the science numbers. Membrane life, power, throughput and recovery cost per kilogram are the business numbers.
Sources and further reading
- Nature — Anodic Pd membrane H₂ extraction enhances thermochemical dehydrogenation
- MIT News — An electrochemical approach turns ammonia into pure hydrogen
- IEA — Global Hydrogen Review 2026, Executive summary
- EU Clean Hydrogen Partnership — COUPLE project
- Air Liquide — Ammonia cracking industrial-scale pilot
- thyssenkrupp Uhde — Ammonia cracking demonstration
- JERA — Hydrogen and ammonia value-chain MoU with Samsung C&T
- KBR — Ammonia cracking unit with ISU Chemical
이 글은 정보 제공 목적이며, 특정 자산의 매수·매도를 권유하지 않습니다.
For information only — this is not a recommendation to buy or sell any asset.
댓글Comments 0